/ KNOWLEDGE · QUALITY
Pass bands for machine health: the five checks that decide whether a moulding machine may run your parts
A moulding machine cannot give you a part that is more repeatable than the machine itself. Rosato counts the machine’s repeatability, with cavity accuracy and mould design, among the three things that decide what comes out of a mould. That is why our quality paper trail puts a machine-health audit beside the inspection reports, and why the standard we publish, KRG-QA-001, writes five checks down with pass bands.
The bands are built on an OEM machine-audit manual of the kind applied to moulding subcontractors, which grades seven items of machine performance. Where a figure below is Kruger’s choice rather than the manual’s, we say so.
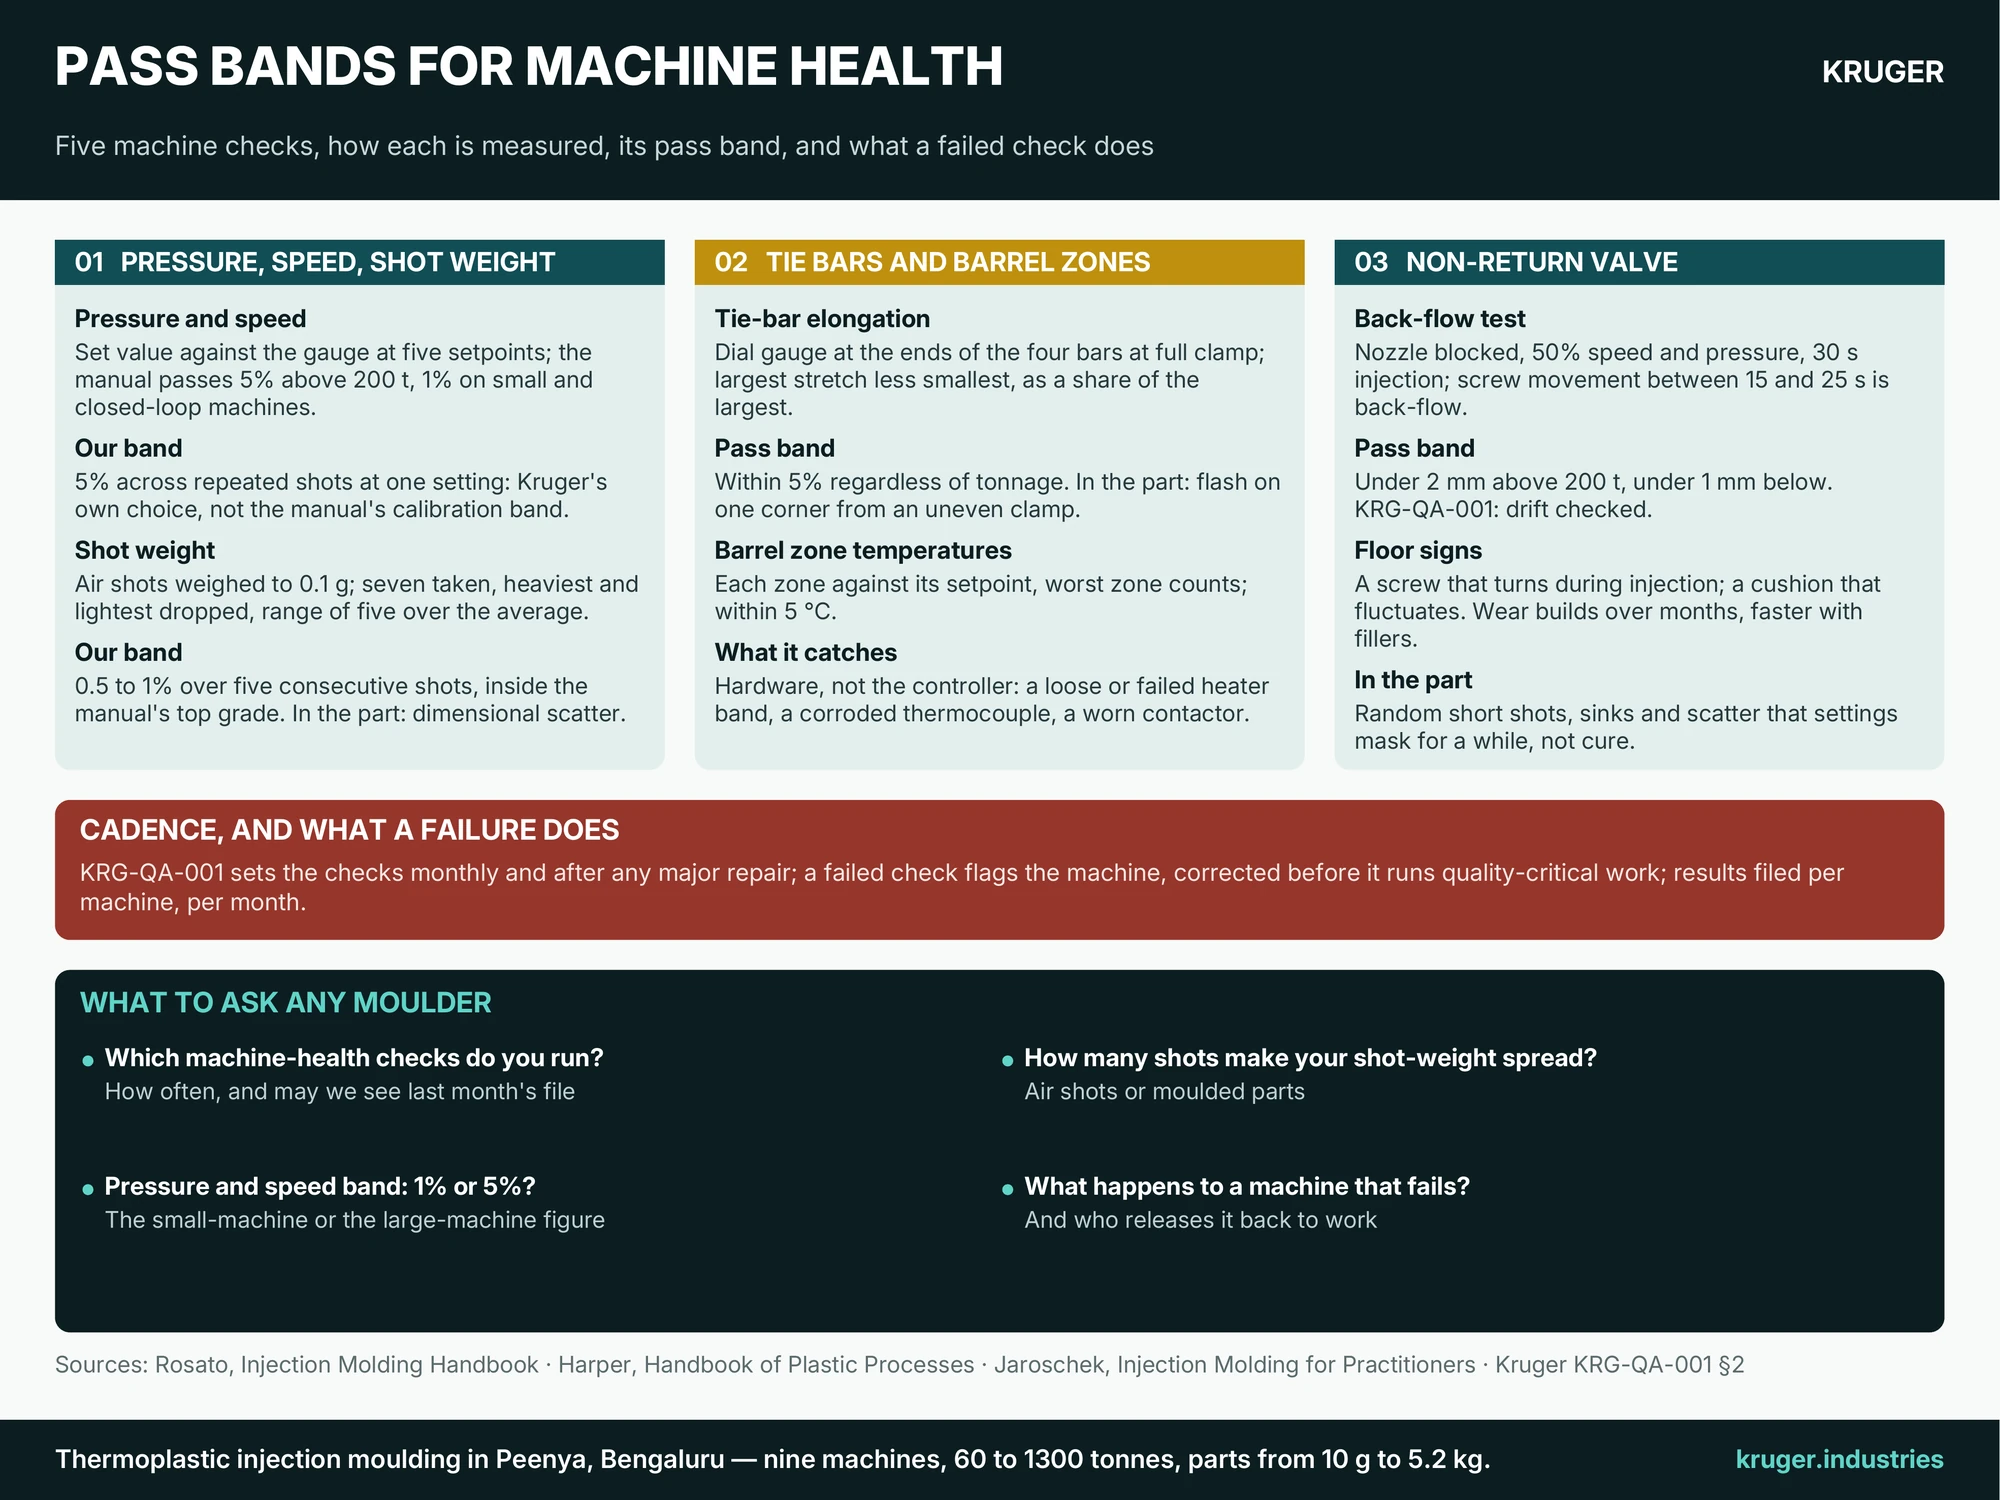
1. Injection pressure and speed
The measure is how faithfully the machine delivers what is set. The manual’s test is a calibration check: holding pressure set at 10, 30, 50, 80 and 99 per cent of maximum hydraulic pressure and each setting compared with the gauge, the 10 per cent point a zero check that is not counted; speed is checked the same way on an empty barrel, as screw travel over injection time. The manual passes under 5 per cent above 200 tonnes, under 1 per cent on smaller and on closed-loop machines. KRG-QA-001 applies 5 per cent to repeated shots at one setting: Kruger’s own band, not the manual’s. Drift comes from valves, pump, controller, lost calibration and a late-closing non-return valve. In the part: short shots and flash from pressure; dull surfaces, flow marks and weld lines from speed.
2. Shot weight
The measure is shot-weight spread, from air shots weighed to 0.1 g. The manual takes seven, discards the heaviest and lightest, and divides the range of the remaining five by their average; its top grade is under 0.5 per cent on small machines and under 1 per cent above 200 tonnes. The band we specify, 0.5 to 1 per cent over five consecutive shots, sits inside that grade. A failed machine is re-tried on 50 moulded parts, each within 1 per cent of average. Drift comes from low back pressure, a worn screw and barrel, and the non-return valve, whose closing behaviour, Jaroschek says, largely sets shot-weight accuracy: about 2 per cent scatter without holding pressure, about 0.2 per cent with it. In the part: dimensional scatter, and with it the tolerance you can hold.
3. Tie-bar elongation
The measure is how evenly the four tie bars stretch at full clamp on a toggle machine: a dial gauge read at the bar ends after high-pressure clamping, with a mould under a year old. The deviation is the largest bar’s stretch less the smallest, as a percentage of the largest. The manual passes under 5 per cent regardless of tonnage, and that is the band we specify; hydraulic clamps are checked on clamping pressure instead, and our toggle clamp page has the mechanics. Drift comes from tie-bar bushes, toggle pins, platens out of parallel and top and bottom bars heating unequally at start-up. In the part: flash on one corner. As our defects guide says, mould rigidity is the commoner cause of flash; an uneven clamp is the machine’s share.
4. Barrel zone temperatures
Each heater zone’s temperature is compared with its setpoint, the worst zone counting. The band is within 5 °C, the manual’s figure, adopted in KRG-QA-001. The manual weights this item lowest, and the handbooks show why: a modern controller holds a zone within a few degrees of setpoint, so more than 5 °C off points to hardware, not the controller: a loose or failed heater band, a corroded thermocouple, a worn contactor. Jaroschek is blunt that barrel temperature does not measure part quality; this is a hardware check. In the part: short shots from a failed band; weld lines, stress and warp from an unstable melt.
5. Non-return valve back-flow
The measure is melt leaking back past the screw tip and check ring under injection pressure, which the manual reads as wear of the screw assembly and barrel. The manual blocks the nozzle, sets 50 per cent speed and pressure and a 30-second injection, and reads screw position at 15 and 25 seconds; the movement between is back-flow, passed under 2 mm above 200 tonnes and under 1 mm below. KRG-QA-001 says drift checked, without a number. Floor signs: Bryce says a screw that turns during injection has a worn or broken ring; Harper watches for rotation once the screw reaches the end of its stroke; a fluctuating cushion reads the same way. Rosato calls a leaking valve “a major cause of shot-to-shot variations”; its wear builds over months, faster with glass and mineral fillers. In the part: random short shots, sinks and scatter that settings mask for a while but do not cure.
Cadence, and what a failure does
The standard we publish, KRG-QA-001, sets these checks monthly and after any major repair. The month is the standard’s rule, not the manual’s, which sets no frequency; it fits what the handbooks observe, that valve wear builds over months and cannot be seen in a short record. KRG-QA-001 puts the consequence in one line: a failed check flags the machine, and it is corrected before it runs quality-critical work; results are filed per machine, per month. It is a gate, not in-run monitoring: Kulkarni shows a leaking ring hiding behind a repeatable hydraulic trace.
What to ask any moulder
- Which machine-health checks do you run, how often, and may we see last month’s file?
- Is your pressure and speed band the small-machine 1 per cent or the large-machine 5 per cent?
- How many shots make your shot-weight spread, air shots or moulded parts?
- What happens to a machine that fails a check, and who releases it?
These extend our supplier qualification guide from the system to the machine; our machines are on the capabilities page. Send us a drawing or a quote request; we will name the machine we would run it on, and you may ask what our machine audits read.
Sources quoted: D. V. Rosato, D. V. Rosato and M. G. Rosato, Injection Molding Handbook, 3rd ed. (Kluwer, 2000); C. A. Harper (ed.), Handbook of Plastic Processes (Wiley, 2006); V. Goodship, ARBURG Practical Guide to Injection Moulding (Rapra, 2004); C. Jaroschek, Injection Molding for Practitioners (Hanser, 2022); S. Kulkarni, Robust Process Development and Scientific Molding, 2nd ed. (Hanser, 2017); D. M. Bryce, Plastic Injection Molding Vol. I (SME, 1996) and Vol. III (SME, 1998). Pass bands and methods: Kruger KRG-QA-001 Rev 1, section 2, built on an OEM machine-audit manual applied to its moulding subcontractors.