
/ KNOWLEDGE · TOOLING
Mould maintenance and storage — who looks after the tool you own?
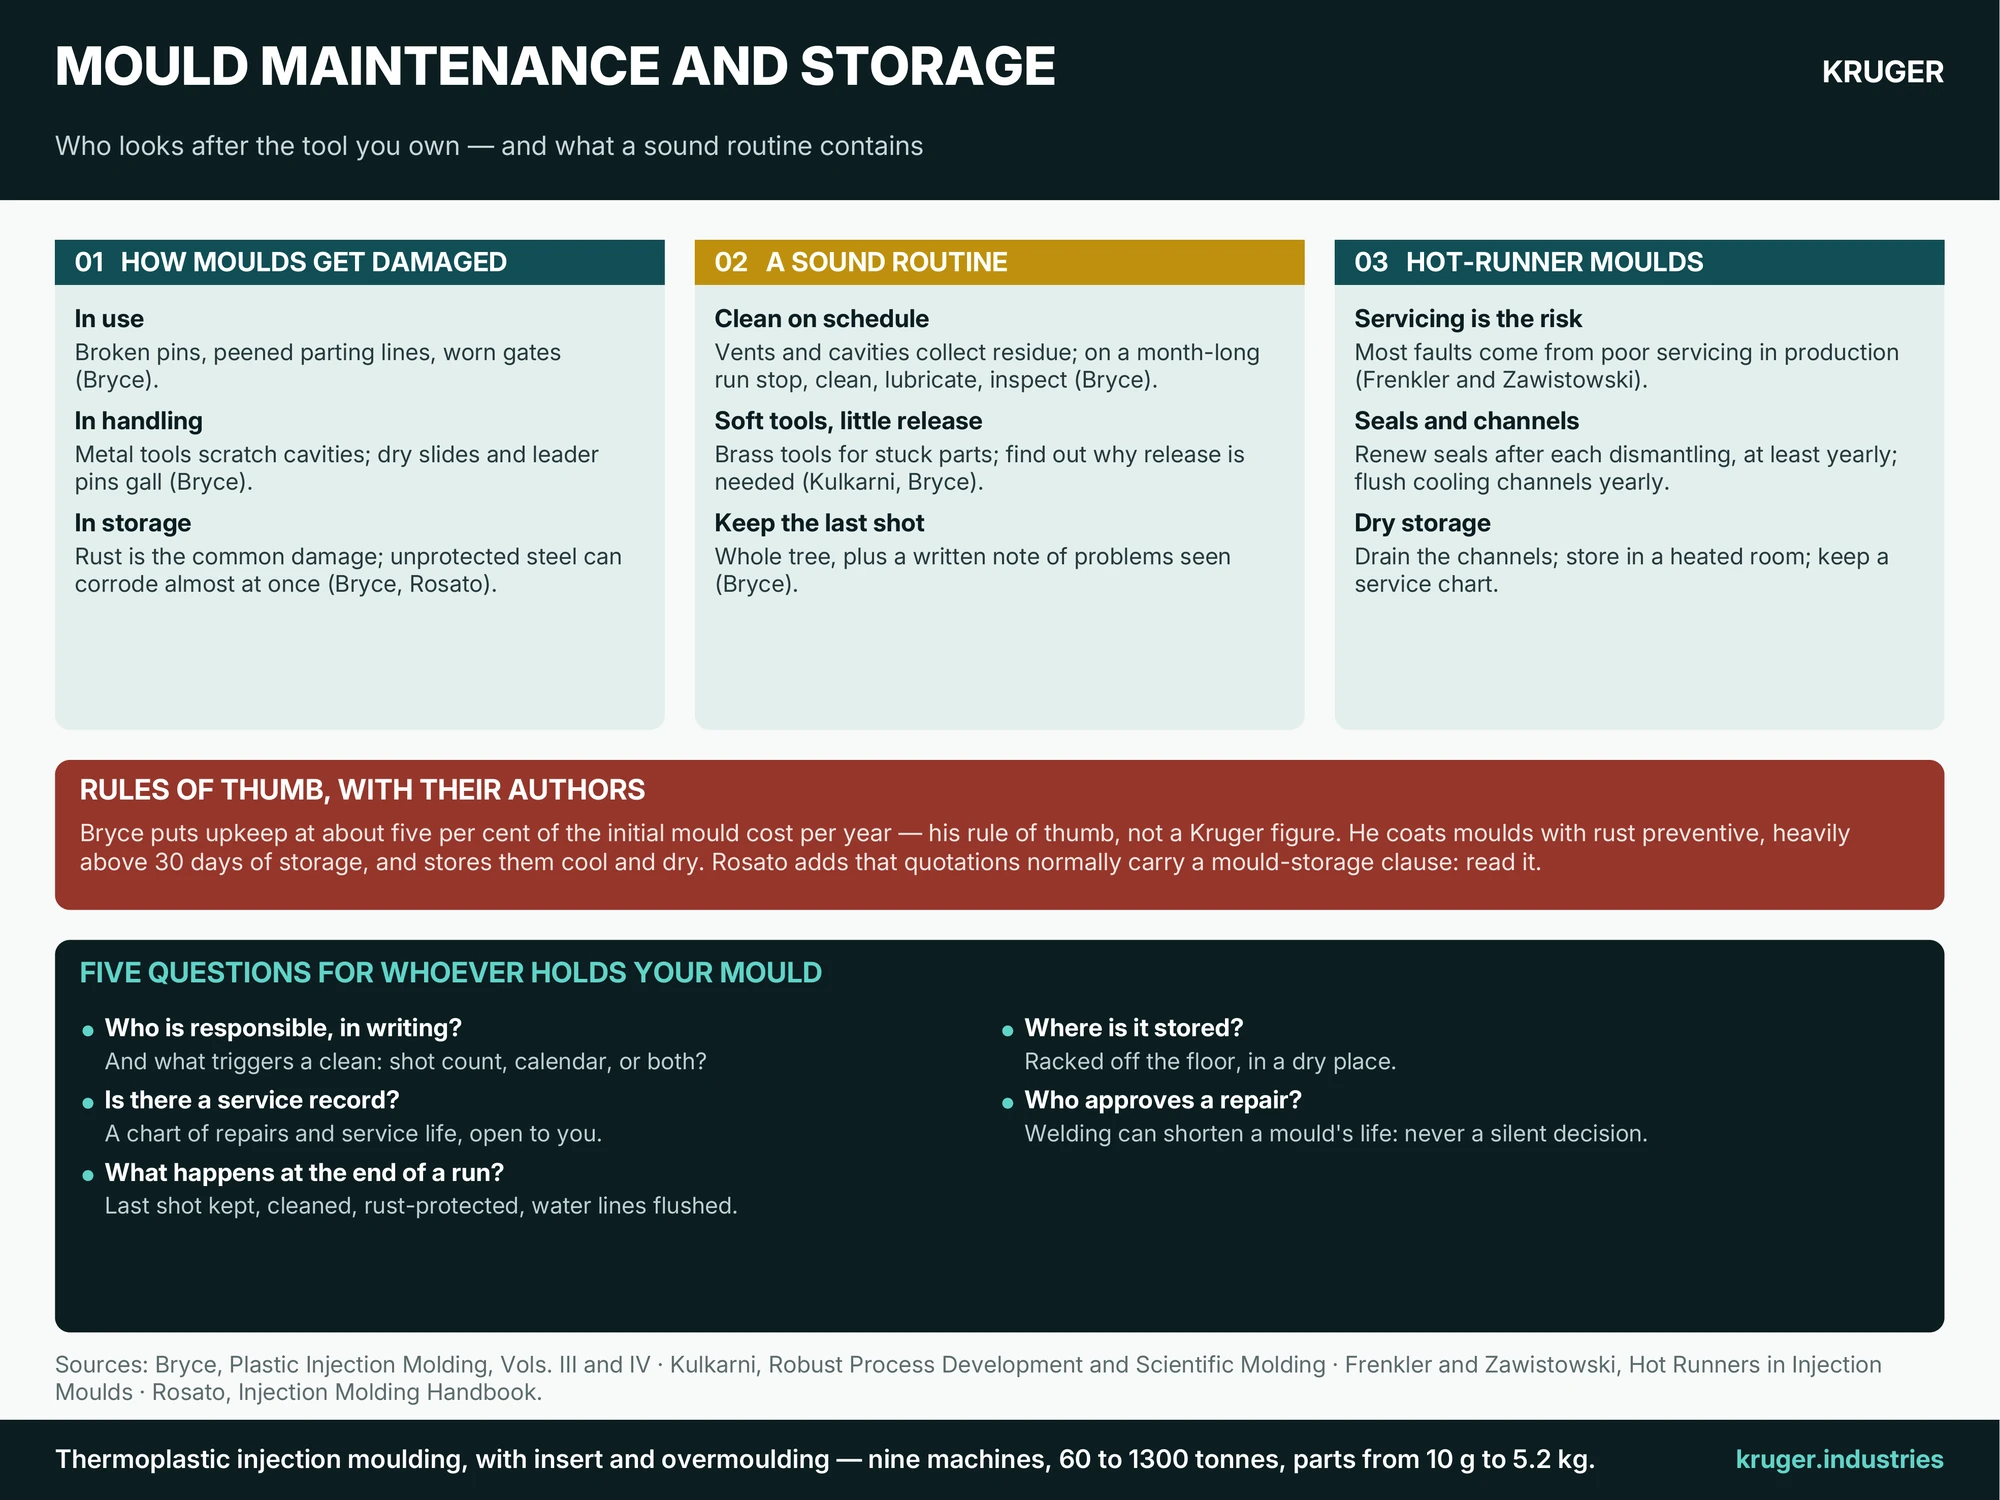
You pay for the mould, but someone else looks after it. In most outsourced moulding the tool belongs to the customer and sits in the moulder’s plant between runs. Bryce describes the split: the investment is usually the customer’s, while the moulder takes on the duty of maintaining the mould in its possession. His rule of thumb, which is not a Kruger figure, is that upkeep averages around five per cent of the mould’s initial cost each year. A tool that is cleaned, lubricated and stored badly costs far more than that, in repairs and in lost production. This page explains how moulds get damaged, what a sound care routine contains, and five questions to ask whoever holds your tool. It pairs with our tooling guide, which sets out who owns what.
How moulds actually get damaged
Bryce sorts the damage into two kinds: in production, snapped core and ejector pins, parting lines hammered out of true and gates worn open; in storage, mainly rust. Much of it is avoidable handling. A metal screwdriver used on a stuck part scratches the cavity, and a scratch can show on every part or act as an undercut that makes later parts stick. Slides, cams and leader pins that are not lubricated gall and eventually seize. Excess injection pressure at start-up flashes the mould, and the flash can lock the mechanisms. Nozzle drool left on the cavity can be crushed when the mould closes. Bryce also warns that temperature differences of more than about 6 °C across a mould risk swelling and galling of the steel, and that residue in the vents forces higher pressure, which invites flash.
What a sound care routine contains
- Cleaning on a schedule. Bryce says a mould should be cleaned after a set number of cycles, with the vents and cavity surfaces collecting most residue. On a long run of about a month he advises stopping the mould to clean, lubricate and inspect it, flush the water lines, check the parting line for peening and the sprue bushing for nicks.
- Soft tools and little release agent. Kulkarni specifies brass or other soft tools for stuck parts and keeps daily mould maintenance as a living record that is updated through production. Bryce discourages mould release and says to find out why it is needed, since it gums up slides, cams and lifters.
- Water flow checked. Kulkarni uses a flow meter during the preventive maintenance schedule so that production flow can later be compared when quality slips.
- A last shot kept. At the end of a run Bryce keeps the final shot, ideally the whole tree, with the mould, plus a written note of problems the operators saw. The repair person then knows what to look for.
Hot-runner moulds need more
A heated manifold adds a second discipline. Frenkler and Zawistowski report that the greatest number of faults, even in good hot-runner systems, comes from poor servicing during production. They advise against operators adjusting temperatures, clearing gates with tools or a flame, or repairing valve pins themselves; seals at the nozzle and manifold contact should be renewed after each dismantling and at least yearly, and cooling channels flushed at least yearly. Because heating elements dislike moisture, the channels should be drained and blown out before storage, ideally in a heated room, and repairs recorded on a chart for the hot runner as for the mould. Our sprue, runner and gate guide covers when a hot runner is worth having, and purging covers changeovers.
Storage and the paperwork around it
Rosato warns that unprotected steel can start to corrode almost at once, so even short-term storage needs protection from water and humidity. Bryce’s routine is to clean and inspect the mould when it leaves the press, coat it with rust preventive, apply it heavily if storage will exceed 30 days, treat the water lines too, and keep the mould somewhere cool and dry. Rosato adds that quotation forms normally carry clauses on indemnification and on who is responsible for mould storage, so read that clause before you accept a quotation. If a tool ever has to move, the mould transfer guide lists the documentation that must travel with it.
Five questions for whoever holds your mould
- Who is responsible in writing, and what triggers a clean — a shot count, a calendar interval, or both?
- Is there a service record for my mould, and can I see it? Frenkler and Zawistowski advise a chart of repairs and service life for the mould and its hot runner.
- What happens at the end of a run? Last shot saved, cleaned, rust-protected, water lines flushed.
- Where is it stored, and is it racked off the floor in a dry place?
- Who approves a repair? Bryce notes that welding can shorten a mould’s life, so a weld should never be a silent decision.
Our guide to the quality paper trail lists the other records that should travel with a lot. Send us your mould details and we will walk through these questions with you.
