/ KNOWLEDGE · MATERIALS
Thermoplastic compounds and moulding grades — what is in the bag, and how to specify it
The word on your drawing is a family. The thing in the bag is a recipe. Nylon 66, polypropylene and ABS each name hundreds of grades that differ in their additives, not their polymer. Osswald defines the subject in one sentence — “The term plastics describes the compound of a polymer with one or more additives” — and Arburg’s practical guide counts more than 18,000 grades in the United States alone, a few additives at several levels each. This guide covers what a compound contains, what each ingredient buys and costs, how a moulding grade differs from an extrusion grade, and how to specify one nobody can swap. Our materials guide covers the families; this page covers the recipe.
What a compound is
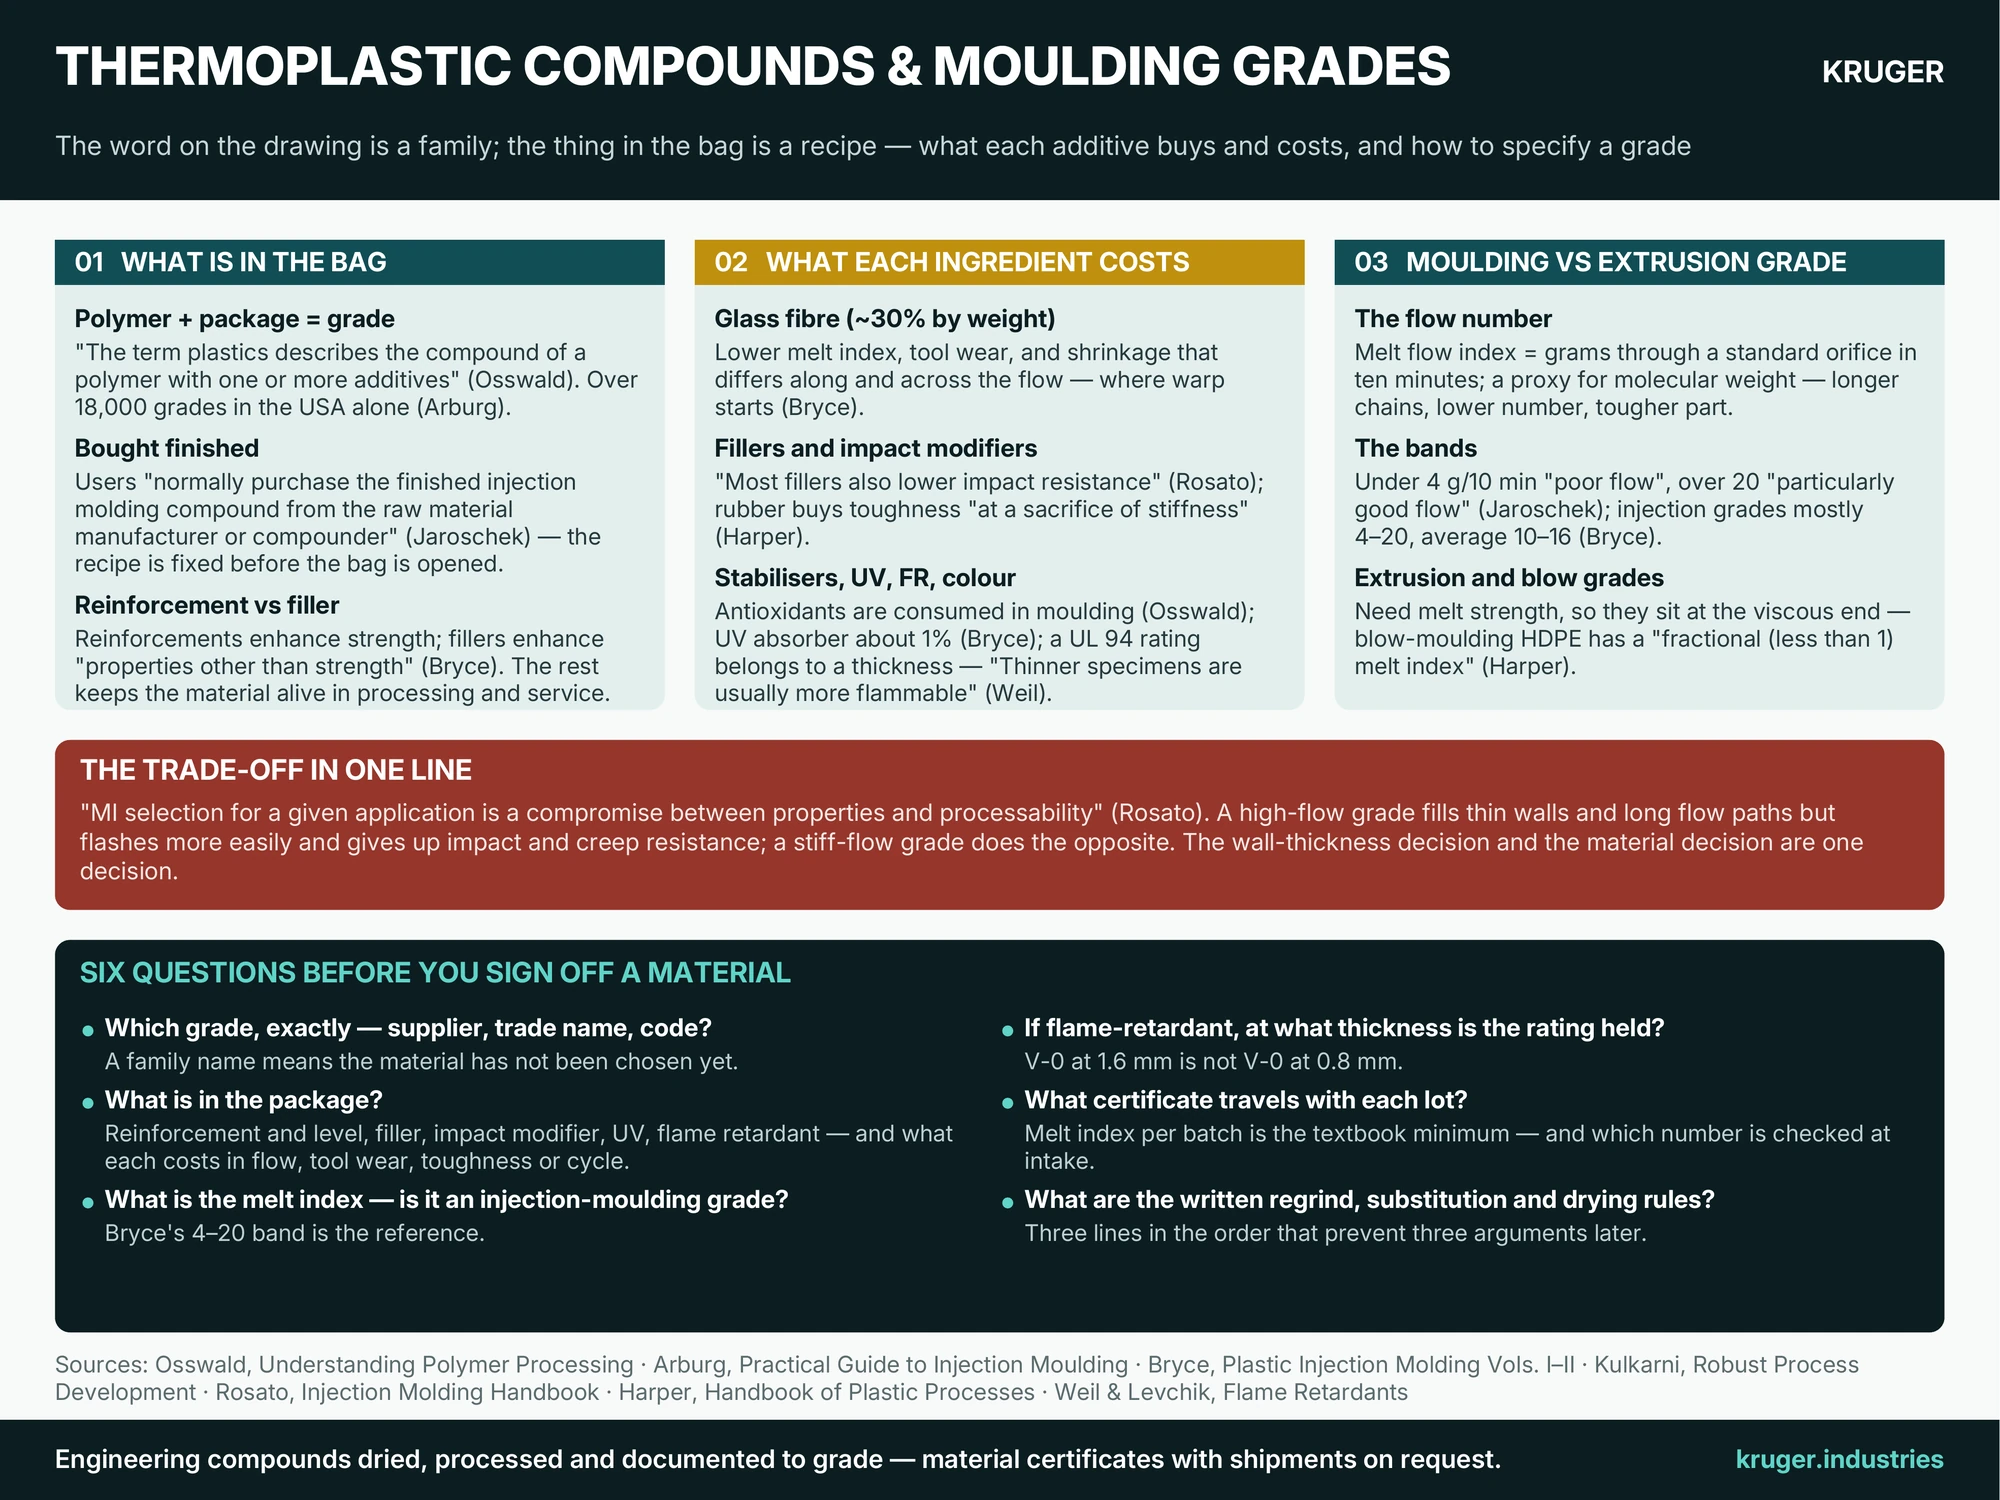
A compound is a base polymer plus a package — reinforcements, fillers, stabilisers, modifiers and colour — melt-blended by the resin maker or a compounder and cut into pellets. Jaroschek’s glossary is clear that the moulder almost always buys the finished compound, so the recipe is settled before the bag is opened and the grade name is all that identifies it. Bryce’s dividing line inside the package: a reinforcement is added for strength, a filler for any other property. The thermoplastics guide covers the base-polymer divide; what follows is the package.
What each ingredient buys — and what it costs
Reinforcement. Glass fibre — Bryce puts typical loading at around 30% by weight — costs three things: flow (Bryce says the melt index usually drops), the tool (fibre wear is his chief worry) and warp, because fibres align with the flow and the part shrinks less along it than across it. The composites guide prices all three. Fillers. Talc and calcium carbonate add stiffness and cut shrinkage, but Rosato is blunt that “Most fillers also lower impact resistance”, and Bryce warns that fillers nearly always add cost and hurt processability — a cheaper bag is not a cheaper part. Impact modifiers. Harper describes the rubber phase as buying impact strength “at a sacrifice of stiffness”. Stabilisers. Antioxidants are consumable: Osswald’s point is that a stabiliser only slows thermal degradation and protection ends once it is used up — so residence time and regrind are material questions. Bryce gives the usual UV-absorber level as about 1% by weight; an outdoor part needs an outdoor grade, not an outdoor hope. Lubricants and release agents. They ease ejection but resist printing and welding; Bryce’s advice is to specify paintable or printable grades where decoration is unavoidable. Flame retardants. Bryce notes that thermoplastics owe their flame retardancy to additives, which cost toughness, and that the rating belongs to the material at a thickness, never to the part — in his words, “Each rating must include mention of the thickness of the test specimens”; Weil’s handbook explains why: thinner bars burn more readily. Colour. Bryce’s rule of thumb for masterbatch is roughly one part in a hundred, and Arburg’s guide requires the carrier to match the base polymer’s melt flow — the colour guide covers the rest.
Moulding grade or extrusion grade — the flow number
Within a family, grades sort first by flow. The melt flow index is the grams of melt pushed through a standard orifice in ten minutes, and it stands in for molecular weight: longer chains, lower number, tougher part. Rosato’s summary is the whole trade-off: “MI selection for a given application is a compromise between properties and processability.” Jaroschek’s glossary calls flow poor below 4 g/10 min and particularly good above 20; Bryce’s experience is that moulding grades usually sit between 4 and 20. Extrusion and blow-moulding grades need melt strength and sit at the viscous end; Kulkarni singles out molecular-weight distribution as “the decisive factor whether a resin is an injection molding grade or an extrusion grade”. In practice a high-flow grade fills thin walls and long paths but flashes more easily and gives up impact and creep resistance; a stiff-flow grade does the opposite. So the wall-thickness guide and the material choice are one decision, and the datasheet guide explains what the number does and does not promise.
Specifying it so the moulder cannot misread it
ABS on a drawing is an invitation to substitute; the ABS guide shows how far two grades sit apart. Write the grade as the compounder names it — supplier, trade name, grade code — because that name is the recipe. Then fix what a name does not. The certificate. Kulkarni notes that MFI is the usual certificate number checked at goods-in; Bryce has the buyer set a window — 13 to 15 in his example — and the supplier certify every batch against it. Ask for it with each lot, because lots vary inside one grade. The substitution rule. Harper warns that two grades of one family, or one grade from two suppliers, can weld and bond quite differently, and datasheets do not rescue you because, as Kulkarni notes, ASTM and ISO values do not convert. So or equivalent should mean a grade approved in writing after trial, not a purchasing convenience. The regrind rule. Bryce’s typical practice is 15% regrind, but a BASF note in Goodship’s troubleshooting collection cautions that engineering thermoplastics tolerate only limited regrind — state your allowance, or zero, in the order; the regrind guide has the clauses. The drying rule. Drying follows the compound, not the polymer: Kulkarni points out that some calcium-based fillers take up moisture, so a filled grade of a non-hygroscopic base still needs the dryer — the drying guide and the temperature chart give the values.
Six questions before you sign off a material
- Which grade, exactly — supplier, trade name, code? A family name means the material has not been chosen yet.
- What is in the package? Reinforcement and level, filler, impact modifier, UV, flame retardant — and what each costs in flow, tool wear, toughness or cycle.
- What is the melt index, and is it an injection-moulding grade? Bryce’s 4–20 band is the reference.
- If it is flame-retardant, at what thickness is the rating held? V-0 at 1.6 mm is not V-0 at 0.8 mm.
- What certificate travels with each lot, and which number is checked at intake? Melt index per batch is the textbook minimum.
- What are the written regrind, substitution and drying rules? Three lines in the order that prevent three arguments later.
We run polypropylene and PPCP, glass-filled polypropylene, polycarbonate, unfilled and glass-filled nylon 6 and 66, ABS, HDPE and PET; engineering compounds are dried, processed and documented to grade, with material certificates available on request. If your drawing still says a family name, send it — an engineer replies within 48 hours on working days with the six questions answered for your part.
Sources quoted: C. A. Harper (ed.), Handbook of Plastic Processes (Wiley, 2006); D. V. Rosato, D. V. Rosato and M. G. Rosato, Injection Molding Handbook, 3rd ed. (Kluwer Academic, 2000); D. M. Bryce, Plastic Injection Molding, Vol. II (Society of Manufacturing Engineers, 1997); T. A. Osswald, Understanding Polymer Processing, 2nd ed. (Hanser, 2017); S. Kulkarni, Robust Process Development and Scientific Molding, 2nd ed. (Hanser, 2017).